Engineered Concealed Slides, Systems & Precision Cabinet Mechanisms
Precision-tested ball-bearing tracks, synchronized undermount slides, and motorized architectural components designed to surpass ANSI/BHMA A156.9 and EN 15338 Grade 1 durability benchmarks.
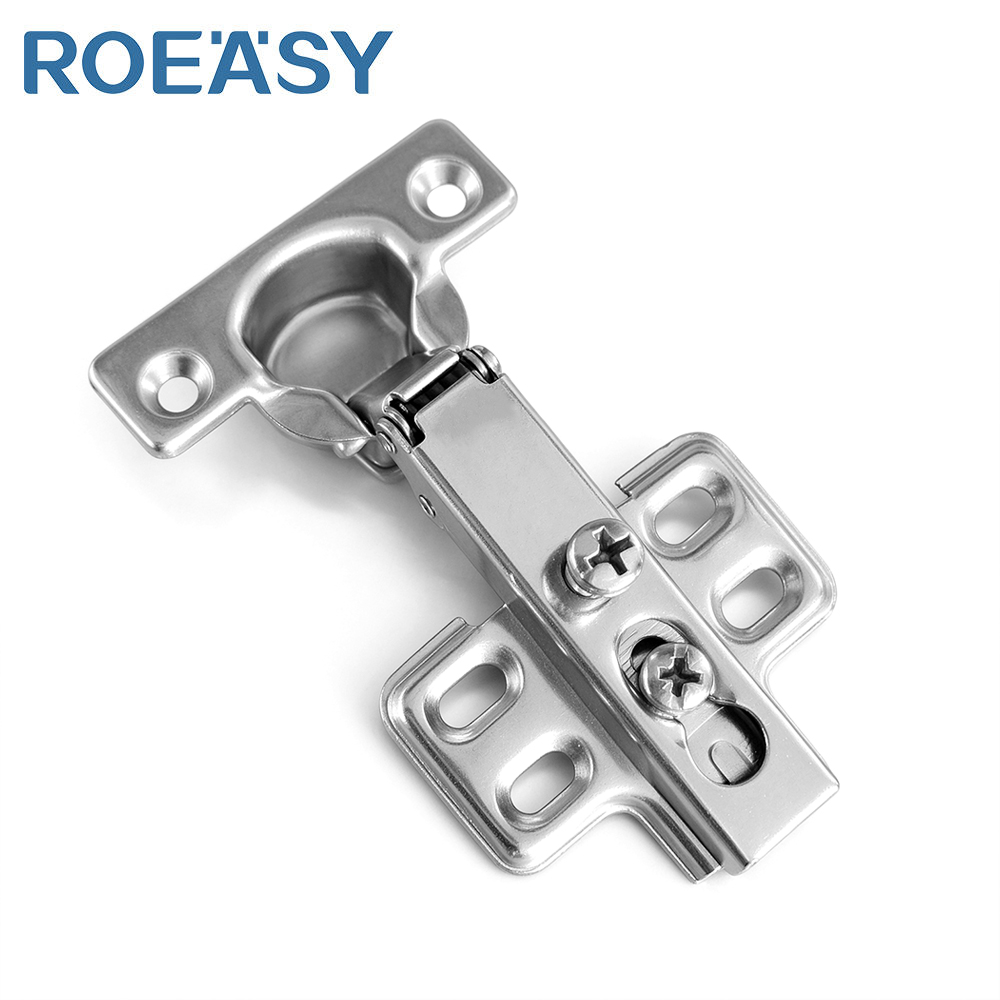
Iron Material Full Overlay One Way 26mm Hinge for Furniture Cupboards Kitchen & Bathroom Cabinets Doors
Cold-rolled steel matrix with continuous nickel coating for high moisture tolerance and structural stability in compact frame cabinets.
Contact Us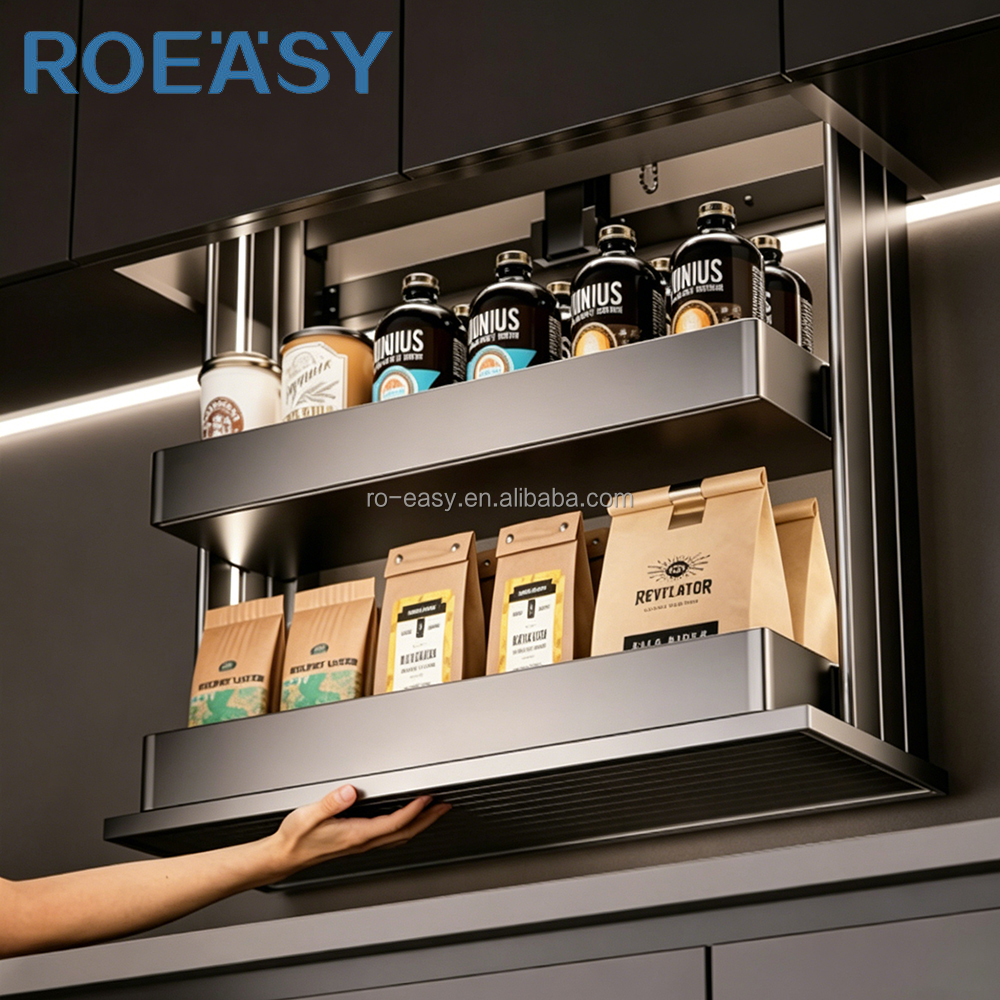
Smart Kitchen Cabinet Lift Electric Vertical Lift System for Upper Cabinets, Motorized Pull Down Shelf for Kitchen Storage
Smart motorized vertical lift kinematics equipped with anti-collision stall detection and silent micro-actuators for handleless upper cabinetry.
Contact Us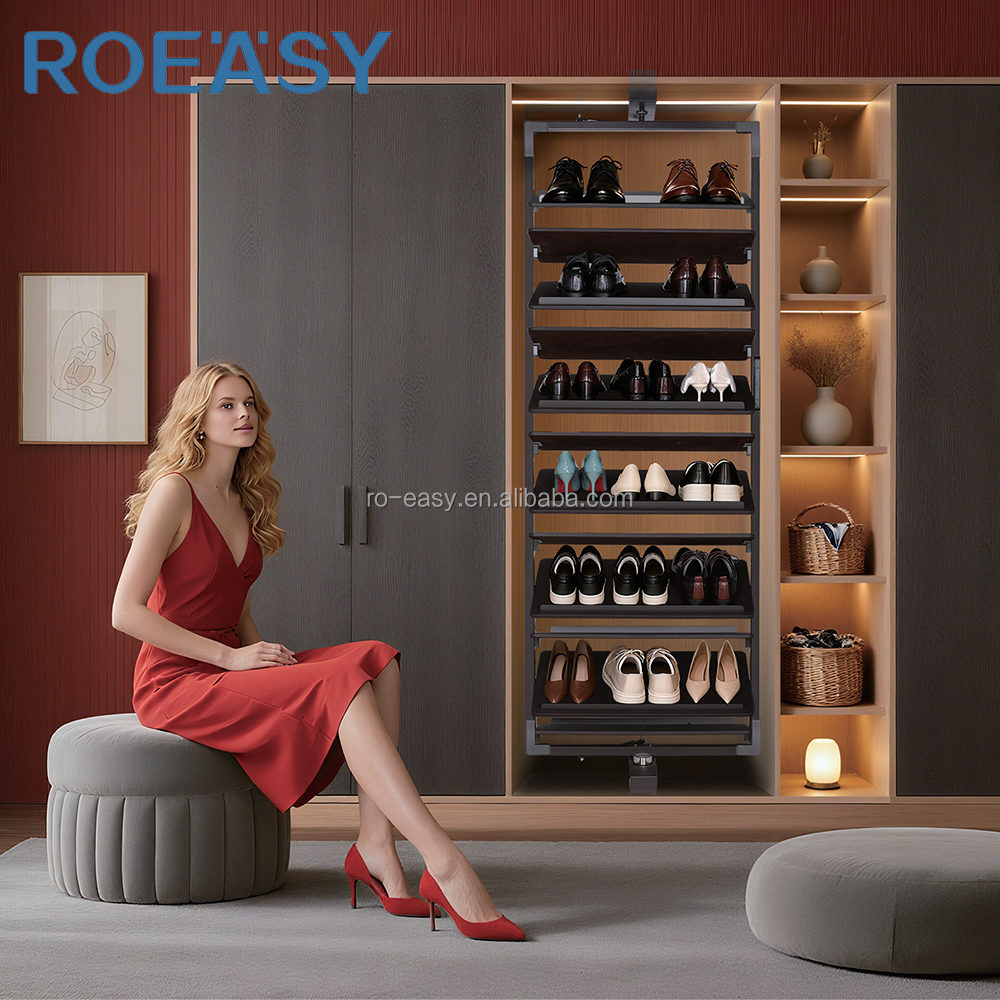
ROEASY KC810 4/6/8/10/12 Tier 360° Revolving Built-in Shoe Rack for Entryway & Walk-in Closet Wardrobe Storage Organizer
Precision engineered ball bearing rotational track mechanism capable of 360-degree high-load radial rotation under extended payload.
Contact Us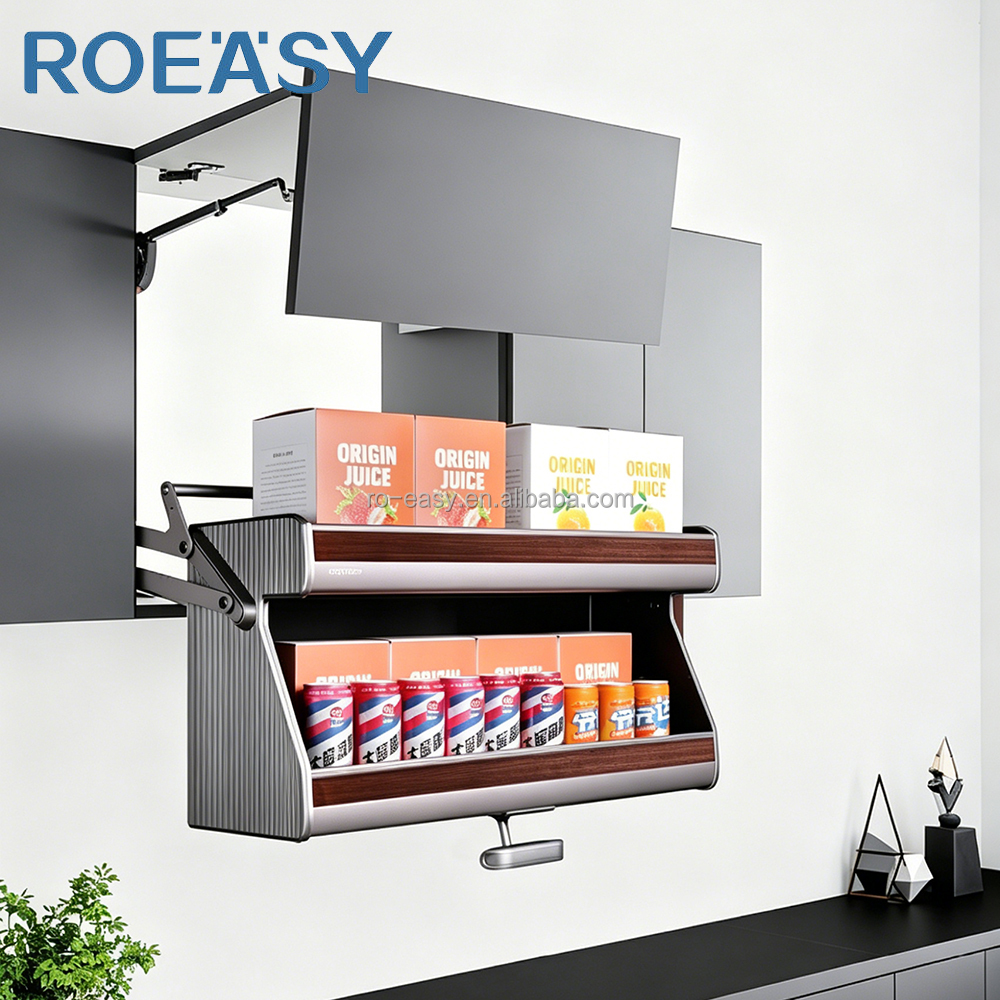
Home Storage Organizer Electric Lifting System Kitchen Cabinet Pull Down Basket Lift
Heavy-load motorized pull-down basket system engineered with balanced dampening guide rails for ergonomic overhead retrieval.
Contact Us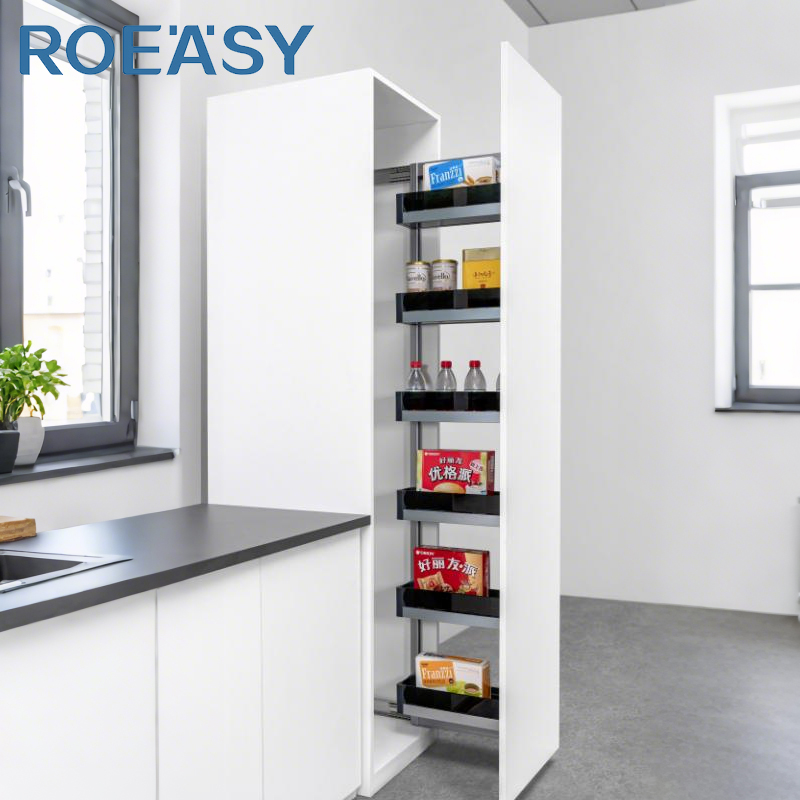
ROEASY Pantry Unit Organizer Kitchen Storage Accessories Modular Cabinet Organization Multi Layer Pull Out Tall Pantry Basket
Heavy-duty synchronized bottom runners coupled with multi-tier link pull-out dynamics designed for high-density vertical pantry storage.
Contact Us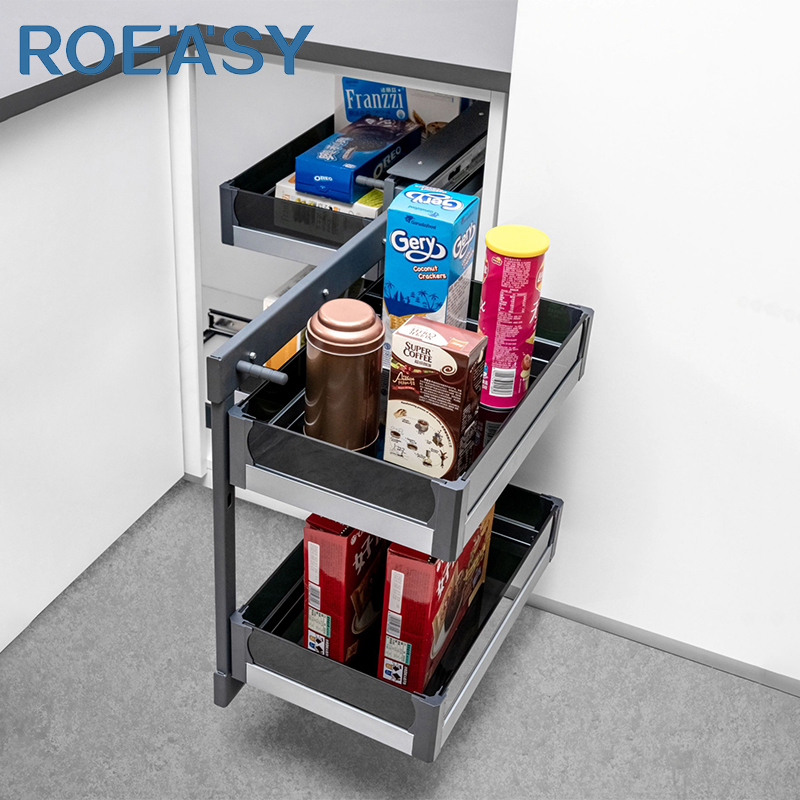
ROEASY Full Extension Magic Corner Basket Spice Rack Kitchen Storage Organizer Cabinet Pantry Kitchen Pull Out Basket
Articulated linkage slide mechanism featuring self-closing buffer dampening, turning blind corner voids into accessible storage spaces.
Contact Us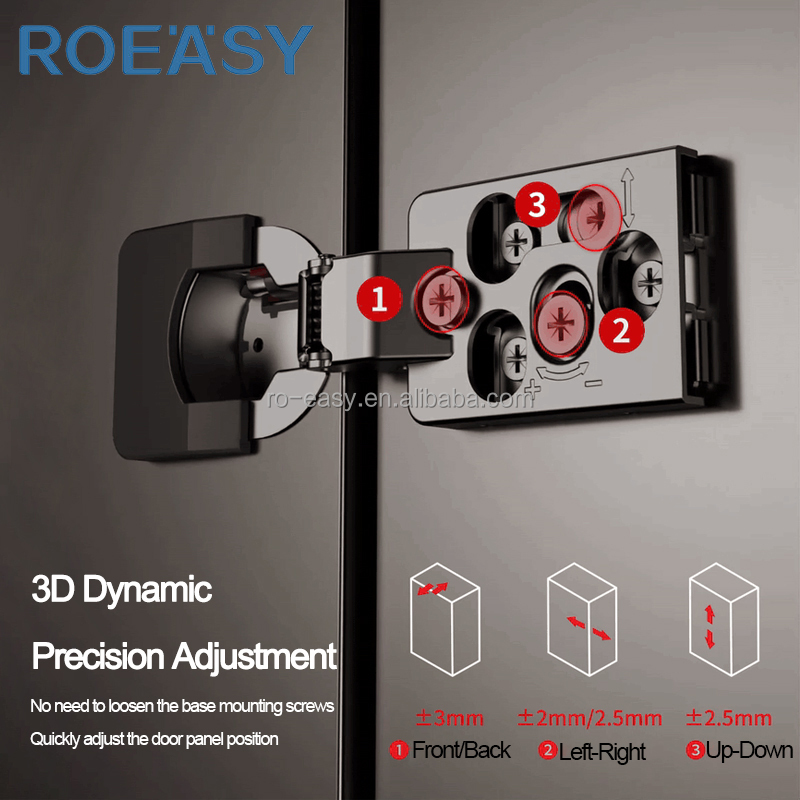
KH05 Ultra Thin Square Flat Design Space-saving 3D Adjustable Hydraulic Soft Close Square Slim Hinge
Ultra-compact planar arm geometry with integrated hydraulic cushioning cylinder and 3D helical adjustment for contemporary minimalist panels.
Contact Us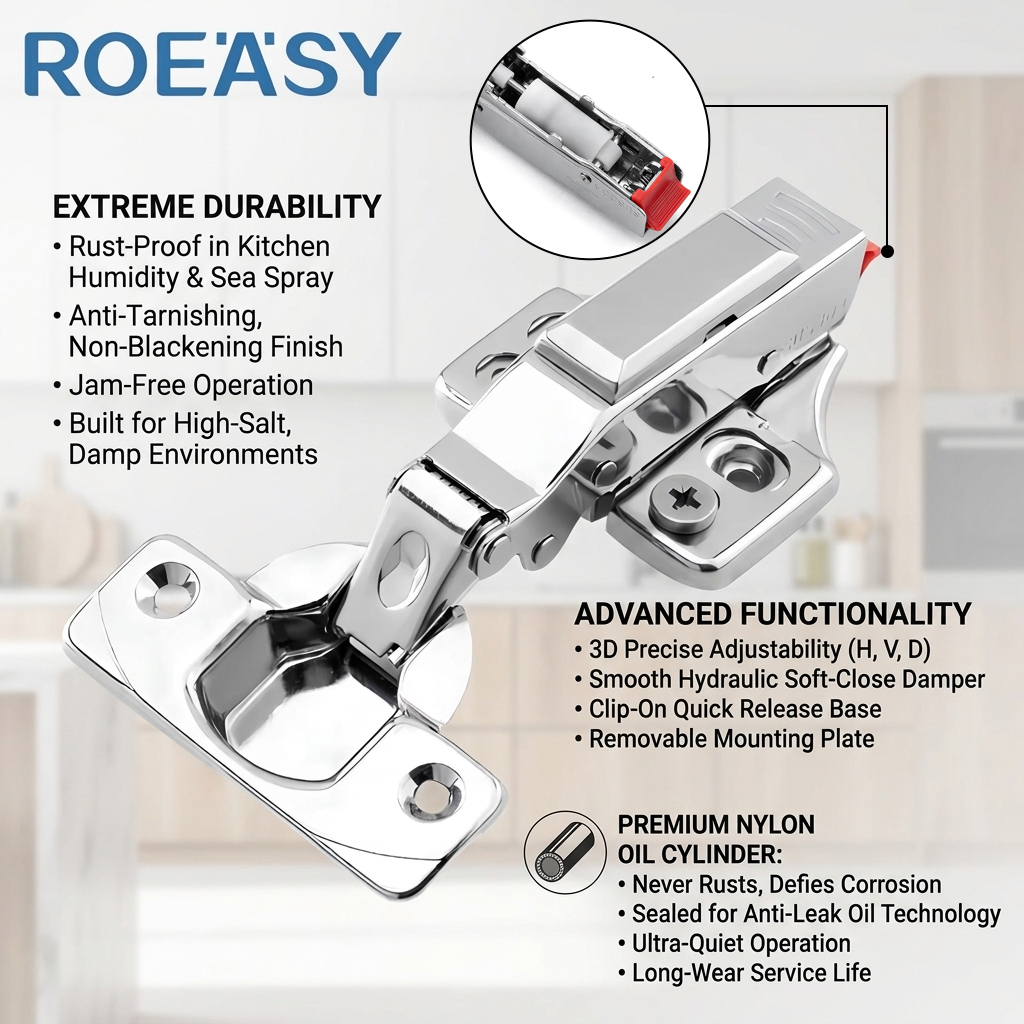
Premium 304 Stainless Steel 3D Hydraulic Soft Close Hinge for Humid Kitchen & Bathroom Cabinets, Coastal Environments
Austenitic SUS304 composition offering extreme resistance against salt-spray corrosion, paired with sealed damping fluid for tropical zones.
Contact UsThe Mechanical Engineering Behind Push-to-Open Drawer Slides
In contemporary architectural cabinet construction, the shift toward clean, handleless aesthetic expressions has elevated the mechanical burden placed on drawer runner kinematics. A push-to-open drawer slide does not simply execute sliding motion; it serves as an energy storage and calibrated release mechanism.
Standard push-to-open slides often suffer from mechanical spring fatigue, latch displacement, or uneven front-panel gap alignment. Professional OEM/ODM manufacturing resolves these physics problems through calibrated dual-spring rebound packs, linear ball tracks stamped from hardened cold-rolled steel, and high-tensile POM (Polyoxymethylene) trip triggers.
By integrating fluid dynamic dampers into the rebound chamber, hybrid systems—often termed "Push-to-Open Soft-Close"—achieve silent kinetic dampening after an energetic ejection stroke, preventing tableware rattle and structural rail warping.
Critical Load-Bearing & Synchronization Parameters
When sourcing push-to-open slides from Chinese manufacturers, technical procurement managers must evaluate several non-negotiable stress tolerances:
Future Sourcing & Procurement Trends in Drawer Slide Engineering
Analysis for hardware importers, system integrators, and custom furniture manufacturers navigating supply chain realignments for 2026–2030.
Consolidated SKU Integration (2-in-1 Systems)
Furniture brands are actively reducing inventory overhead by procuring hybrid runner assemblies that integrate push-to-open and fluid-damped soft-closing functions into a single SKU. This eliminates split inventory lines and provides field flexibility during installation.
Thin-Wall Drawer Box Co-Development
Procurement is moving away from standalone bottom-mount slides toward integrated ultra-slim metal drawer box systems (such as 13mm double-wall profiles). Buyers source coordinated sets where the push-to-open slide runners are calibrated to the weight and dampening response of the steel sides.
Stringent Green Metallurgy Standards
With carbon border taxes and circular product mandates taking root across Europe and North America, OEM clients are auditing steel mills directly. Low-carbon recycled cold-rolled steel, waterborne degreasing treatments, and toxic-free electroplating are becoming prerequisites for global tenders.
Push-to-Open Mechanism Comparative Engineering Matrix
| Mechanical Parameter | Commercial Grade (Standard OEM) | Premium Architectural (Heavy Duty) | Synchronized Slim Box System |
|---|---|---|---|
| Mounting Configuration | Side-Mounted 45mm Ball Bearing | Concealed Undermount 3-Fold Runner | Integrated Slim Double-Wall Profile |
| Dynamic Load Rating | 25 kg – 35 kg (55 lbs - 77 lbs) | 40 kg – 50 kg (88 lbs - 110 lbs) | 40 kg – 60 kg (Standard/Expanded) |
| Fatigue Cycling Benchmark | 30,000 Cycles (GB/T standard) | 50,000 – 80,000 Cycles (ANSI/BHMA A156.9) | 100,000 Cycles (EN 15338 Level 3) |
| Trigger Gap Tolerance | 3.5 mm – 5.0 mm required gap | 2.0 mm – 3.0 mm calibrated trigger | 1.5 mm – 2.0 mm ultra-tight gap |
| Wide Drawer Stability | Susceptible to racking over 600mm | Compatible with optional cross-link rod | Built-in dual-pinion synchronization standard |
| Adjustment Matrix | 1D Height Adjustment via Cam | 2D / 3D Tool-Free Ergonomic Locking Clips | Integrated 3D Internal Adjustment (±2mm) |
Verified Britton Hardware Industrial Infrastructure
Direct manufacturer capabilities verified onsite by SGS Group, providing resilient capacity for high-volume custom production.
Operating two specialized manufacturing facilities across Shantou (Chenghai) and Zhaoqing (Gaoyao), covering high-speed continuous progressive metal stamping, plastic injection molding, and robotic sub-assembly lines over 20,000 square meters of production area.
Equipped with computerized hinge cyclic durability testers, guide-rail continuous fatigue apparatus, pneumatic load calibrators, neutral salt spray chambers, digital Rockwell hardness gauges, and falling-ball impact test apparatus ensuring complete batch traceability.
Our in-house tooling and design engineering group delivers end-to-end OEM/ODM execution—transforming 3D CAD step files and rapid functional prototypes into mass production tooling within 25 to 35 working days, including custom laser marking and packaging.
Frequently Asked Questions on Push-to-Open Drawer Hardware Sourcing
How do push-to-open slides handle wide or asymmetrical pull-out loads?
Drawers wider than 600mm generate off-axis torque when pressed on either the far-left or far-right corner. To eliminate racking or mechanism lock-up, reliable OEM suppliers implement a transverse synchronization rod coupled with dual rack-and-pinion gearings. This mechanically equalizes the push stroke across both slide channels, allowing activation from any touchpoint across a 1200mm front panel.
What causes push-to-open slides to fail premature endurance tests?
Premature failure typically stems from three mechanical vulnerabilities: spring fatigue in the ejection pack, degradation of the plastic latch track due to friction heat or brittle resin selection, and rail misalignment from soft steel grades. Britton Hardware utilizes oil-tempered alloy spring wire, self-lubricating DuPont POM molded trigger cams, and high-tensile Q235 cold-rolled steel channels to ensure steady operation beyond 50,000 cycles.
What is the typical Minimum Order Quantity (MOQ) and production lead time?
For standard production models of ball bearing and concealed undermount push-to-open slides, MOQs generally start from 500 to 1,000 pairs, or 1,200 to 7,500 inches for ball-bearing series. Custom ODM programs involving proprietary tooling require minimum runs between 3,000 and 5,000 pairs. Standard factory lead time ranges from 25 to 35 calendar days following pilot sample verification.
Can the push-trigger tension be calibrated for varying drawer weights?
Yes. Premium undermount push-to-open assemblies feature multi-stage adjustable tensioners on the locking clips or rear dampening blocks. This allows installers or end users to adjust the rebound force based on whether the drawer carries lightweight cutlery or heavy cookware, maintaining a uniform 2mm gap reveal.
What certifications and testing reports should buyers request before container loading?
Importers should require full batch documentation including ISO 9227 Neutral Salt Spray (NSS) test certifications (minimum 48-hour rating without corrosion), ANSI/BHMA A156.9 or EN 15338 Grade 1/Grade 3 dynamic load fatigue test reports, RoHS/REACH compliance paperwork for plastic and lubricant components, and SGS factory audit verification reports.
Accelerate Your Custom Hardware Program with a Direct Factory Partner
Consult with our engineering team for technical CAD drawings, sample validation packs, load calculations, and competitive OEM/ODM production quotes.
Contact Us